Bleacher for Edible Oil Refinery
Vacuum-based bleaching systems engineered to strip color pigments, trace metals, and residual soap from neutralized oil, delivering clear, oxidation-resistant oil ready for deodorization.
Bleaching Equipment
(Vacuum Bleacher)
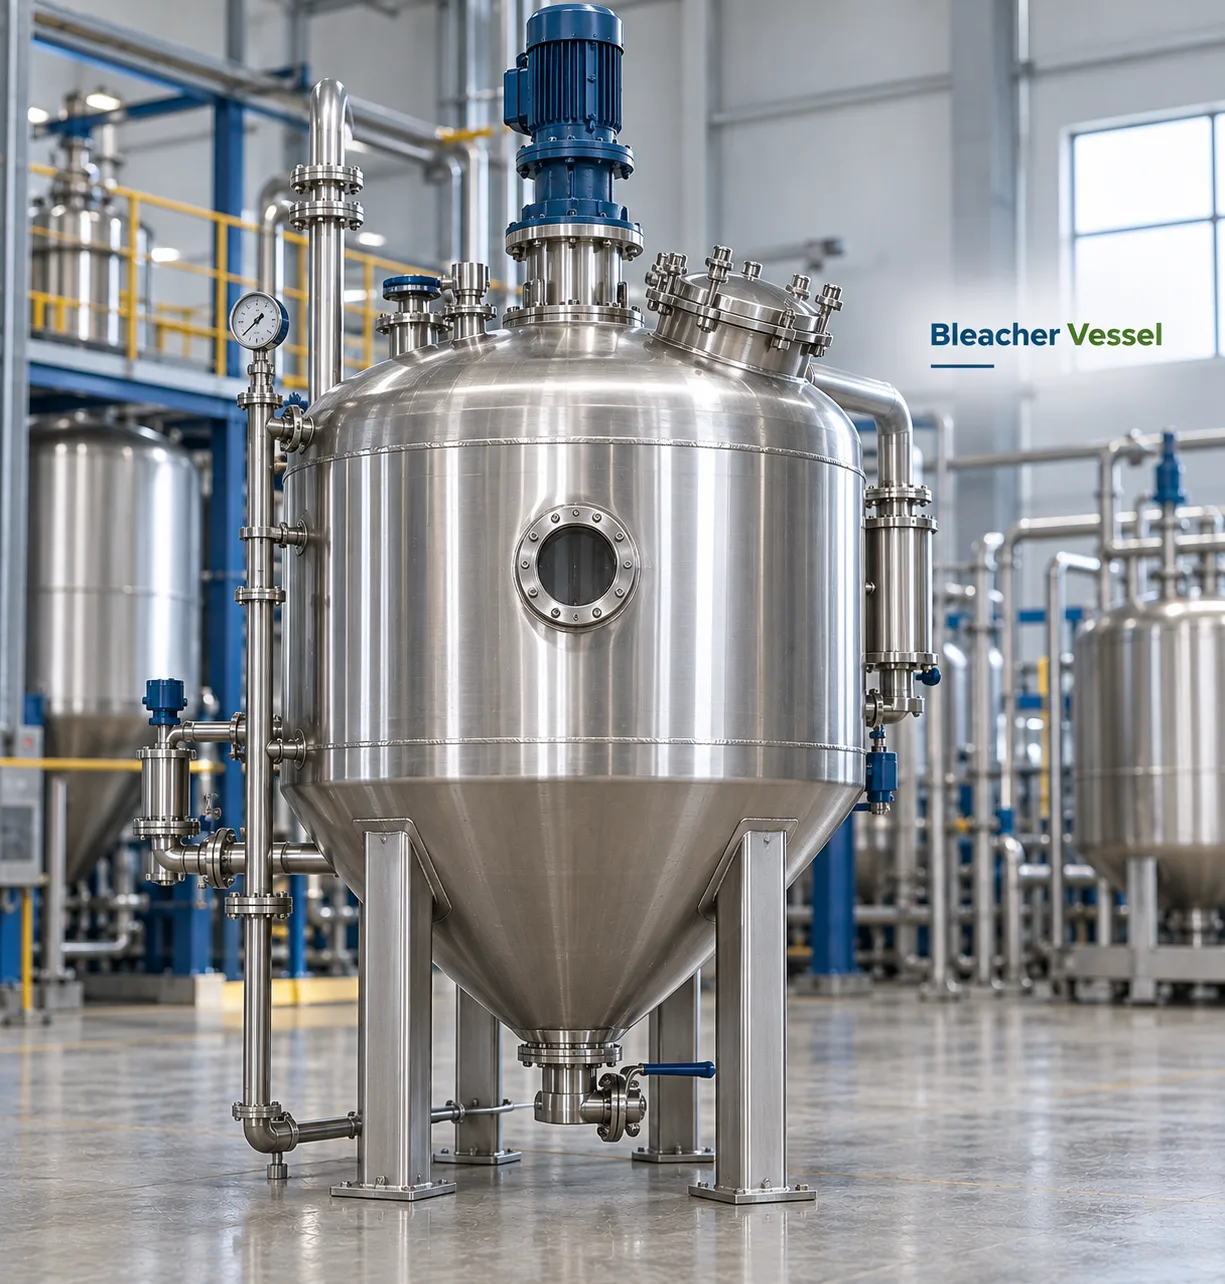
Super Techno Engineers' Bleacher for Edible Oil Refinery is edible oil bleaching equipment built around a precisely dosed and mixed bleaching earth slurry process. Neutralized, dried oil is heated under vacuum and mixed with activated bleaching earth in the bleacher vessel, where the earth adsorbs color pigments, trace metals, residual soap, and oxidation by-products carried over from earlier refining stages. The spent earth is then filtered out through a dedicated bleaching earth filtration system, leaving behind clear, light-coloured oil ready for deodorization.
As edible oil bleaching plant requirements vary by capacity and product mix, our systems are available as either a batch type edible oil bleacher for smaller and mid-scale operations, or a continuous edible oil bleaching plant for high-throughput, round-the-clock refining lines.
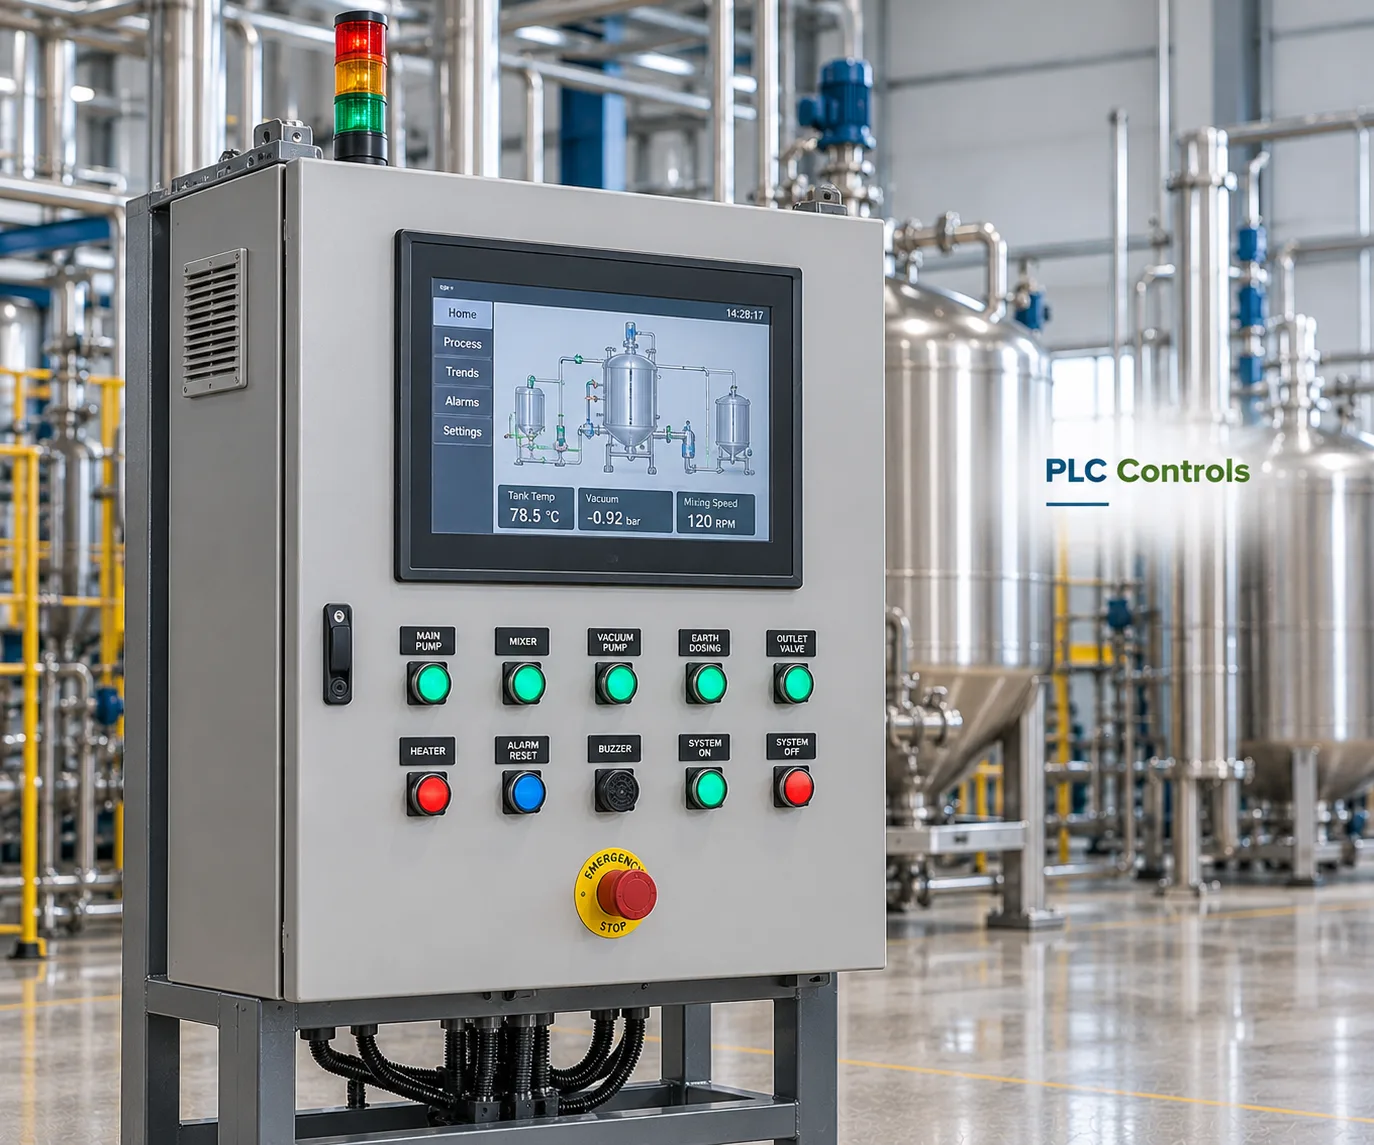

Vacuum Bleaching & Earth Dosing Control
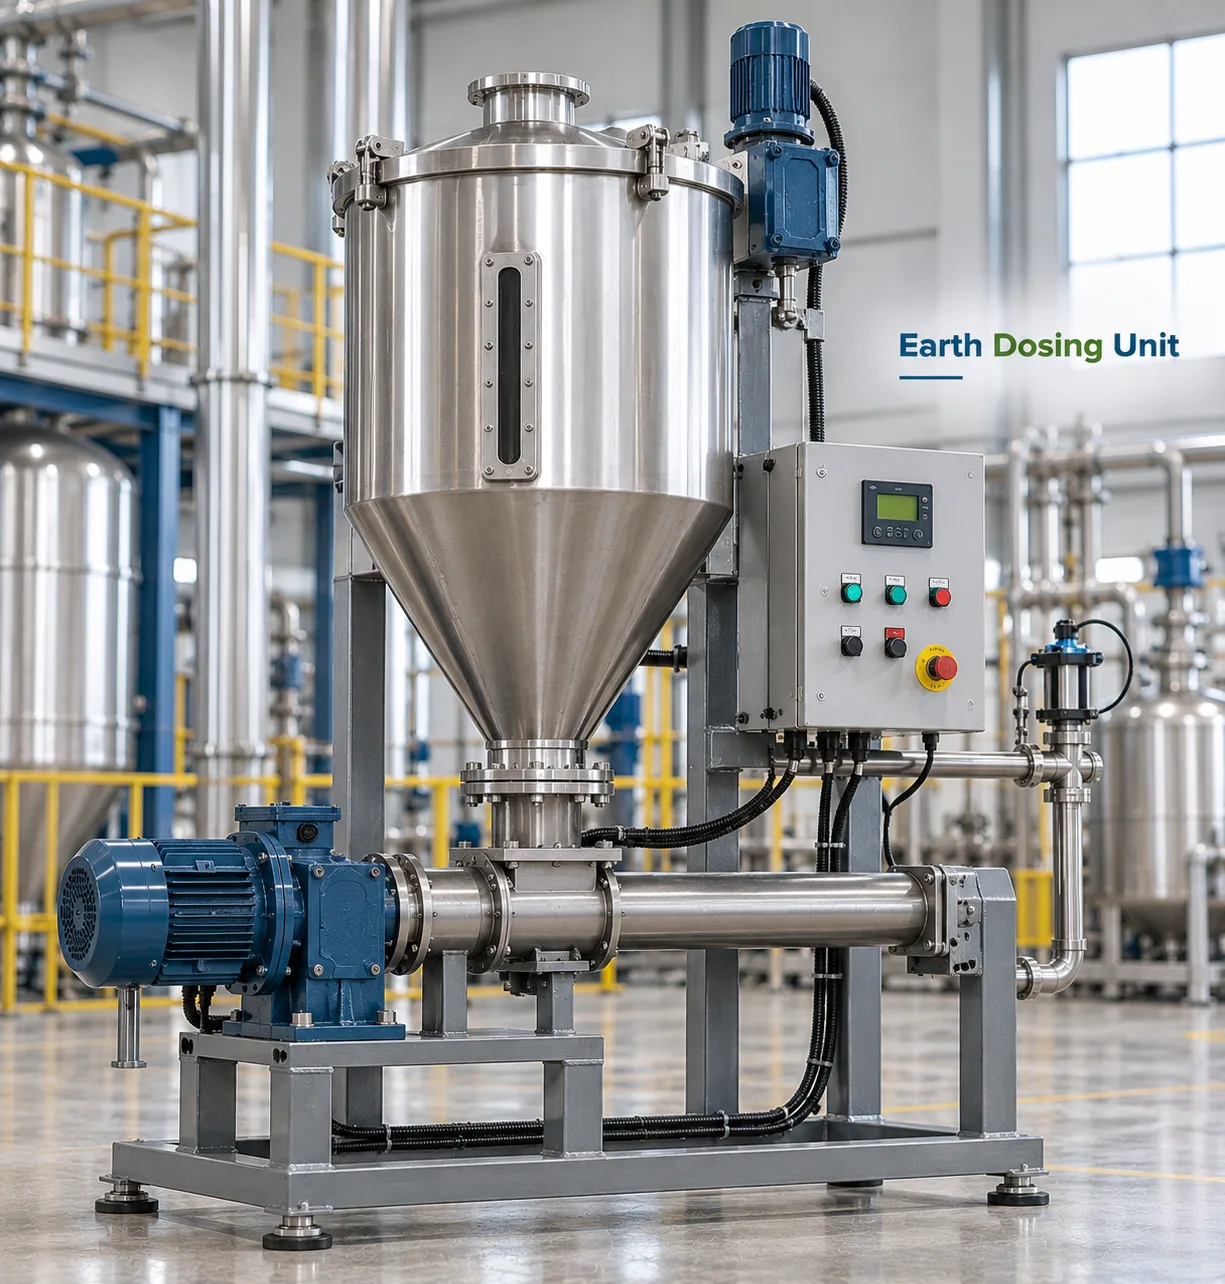
The core of an effective edible oil bleaching process is maintaining the correct combination of vacuum level, temperature, and bleaching earth dosage for the specific crude oil colour and impurity load entering the bleacher. Our vacuum bleacher for edible oil is designed with a dedicated mixing and contact section, allowing the oil-earth slurry sufficient residence time for maximum pigment adsorption before filtration.
Operating under vacuum throughout the bleaching cycle protects the oil from oxidation and limits colour reversion, which is critical for oil that will later pass through high-temperature deodorization.
-
check_circlePrecise bleaching earth dosing calibrated to incoming oil colour and phosphorus carryover.
-
check_circleVacuum-tight vessel design to minimize oxidation during the bleaching cycle.
-
check_circleEfficient mixing section for maximum contact time between oil and bleaching earth.
Built for Continuous Vacuum Operation
Our edible oil bleaching machine is fabricated from heavy-gauge carbon steel or stainless steel, with all product-contact surfaces in stainless steel to prevent contamination and support long-term hygienic operation. The vessel is engineered to hold vacuum consistently across extended production runs, since any loss of vacuum integrity directly affects bleaching efficiency and finished oil colour.
Internal spray nozzles, earth dosing systems, and mixing elements are built for continuous exposure to bleaching earth slurry without excessive wear, keeping maintenance intervals predictable across both batch and continuous configurations.
Operational Capabilities
Performance Highlights
Delivers consistently light-coloured oil by adsorbing pigments, trace metals, and residual soap.
Available as a batch type bleacher or a continuous plant to match your production scale.
Precisely controlled dosing keeps bleaching earth usage aligned with incoming oil quality.
Technical Specifications
Engineered Features
Vacuum-tight bleacher vessel engineered specifically for oxidation-protected processing, preserving oil quality during bleaching.
Precision bleaching earth dosing system accurately calibrated to incoming oil colour and specific impurity loads.
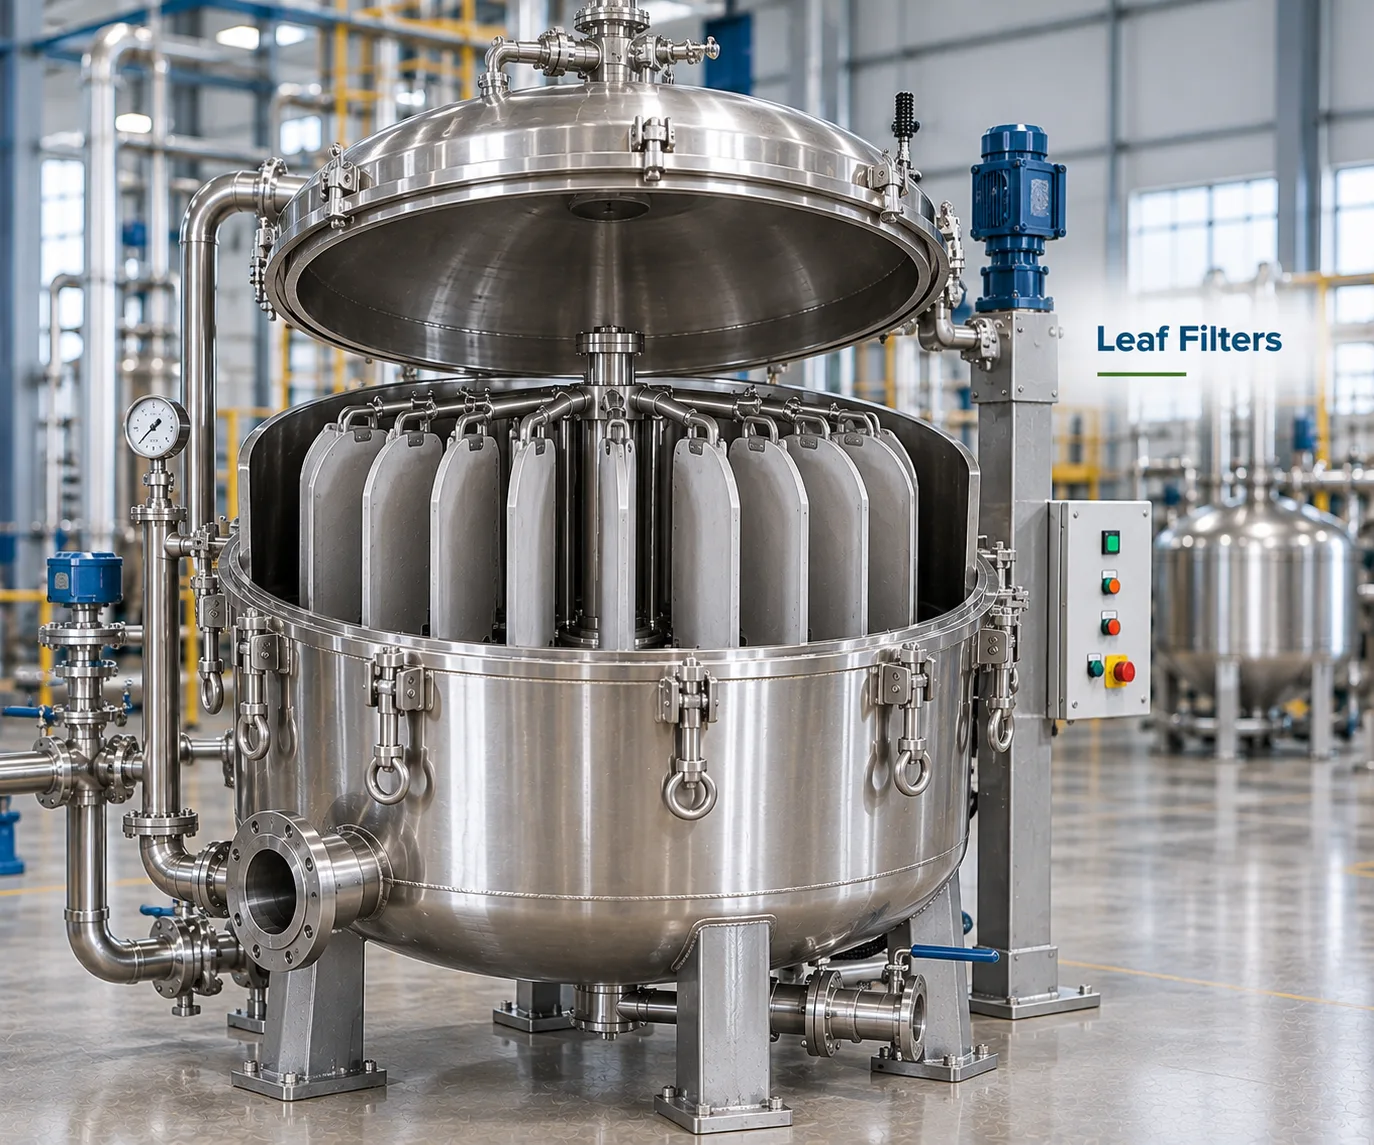
Integrated bleaching earth filtration system specifically designed for thorough and efficient spent earth removal.
Equipped with PLC-based control for continuous monitoring and management of temperature, vacuum levels, and mixing time.
Available in both batch or continuous configuration options to perfectly align with your specific plant requirements.
Heavy-gauge, corrosion-resistant construction designed for long operational life even under rigorous refining conditions.
Data Sheet
Standard Specifications
Comprehensive technical parameters for our Bleacher for Edible Oil Refinery. Custom configurations are available upon request.
| Parameter | Description / Value |
|---|---|
| Plant Capacity | 20 TPD to 1000 TPD (Tonnes Per Day) |
| Configuration | Batch Type or Continuous Edible Oil Bleaching Plant |
| Bleaching Agent | Activated Bleaching Earth (Clay) |
| Earth Consumption | 8-12 Kg per Ton of oil processed (typical) |
| Operating Condition | High Vacuum, Controlled Temperature |
| Filtration | Bleaching Earth Filtration System (Leaf Filters) |
| Material of Construction | Carbon Steel / Stainless Steel (product-contact parts) |
Implementation Protocol
How We Work
Our engineering teams size every Bleacher for Edible Oil Refinery to match your neutralized oil's colour, impurity load, and target throughput.
Feed & Colour Analysis
We evaluate your neutralized oil's colour, phosphorus and soap carryover, and required final specification to determine bleaching earth dosage and vessel sizing.
Vacuum & Dosing Design
Our engineers calculate the optimum vacuum level, temperature profile, and earth dosing system to achieve consistent colour reduction with minimal clay consumption.
Fabrication & Testing
The bleacher vessel, mixing section, and filtration system are fabricated, vacuum-tested, and assembled before shipment and integration into your edible oil refining line.
Value Proposition
Why Choose Our Bleacher
Trusted Bleacher Manufacturer
As an established bleacher manufacturer for edible oil, Super Techno Engineers has delivered bleaching equipment to processors across Indian and international markets.
Batch or Continuous Choice
We supply both a batch type edible oil bleacher for flexible operations and a continuous edible oil bleaching plant for high-volume, round-the-clock refining lines.
Optimized Earth Filtration
Our integrated bleaching earth filtration system ensures thorough spent earth removal, protecting downstream deodorization equipment from carryover impurities.
Complete Turnkey Support
We deliver the complete plant as a single-point turnkey solution, from process design and equipment manufacturing to installation, commissioning, and after-sales.
ISO 9001:2015 Certified
Every component of our edible oil bleaching machine is manufactured under ISO 9001:2015 certified processes, ensuring consistent quality and long operational life.
Seamless Integration
Our vacuum bleacher connects directly with upstream neutralization and downstream deodorization sections, supporting a complete, single-vendor refining line.
Support & Information
Frequently Asked Questions
The edible oil bleaching process removes colour pigments, trace metals, residual soap, and oxidation by-products that remain in the oil after degumming and neutralization, using activated bleaching earth under vacuum.
A batch type edible oil bleacher suits smaller or variable production volumes, while a continuous edible oil bleaching plant is better suited to high-volume, round-the-clock refining operations.
Operating the vacuum bleacher for edible oil under vacuum protects the oil from oxidation during the bleaching cycle, preventing colour reversion and preserving oil quality ahead of deodorization.
After the oil-earth slurry has had sufficient contact time, it passes through a bleaching earth filtration system, typically leaf filters, which separate the spent earth and leave clear, light-coloured oil.
Bleaching earth dosage depends on the incoming oil's colour, phosphorus and soap carryover from earlier refining stages, and the target colour specification for the finished oil.
Super Techno Engineers offers edible oil bleaching plant configurations from 20 TPD for smaller processors up to 1000 TPD for large-scale, continuous commercial operations.